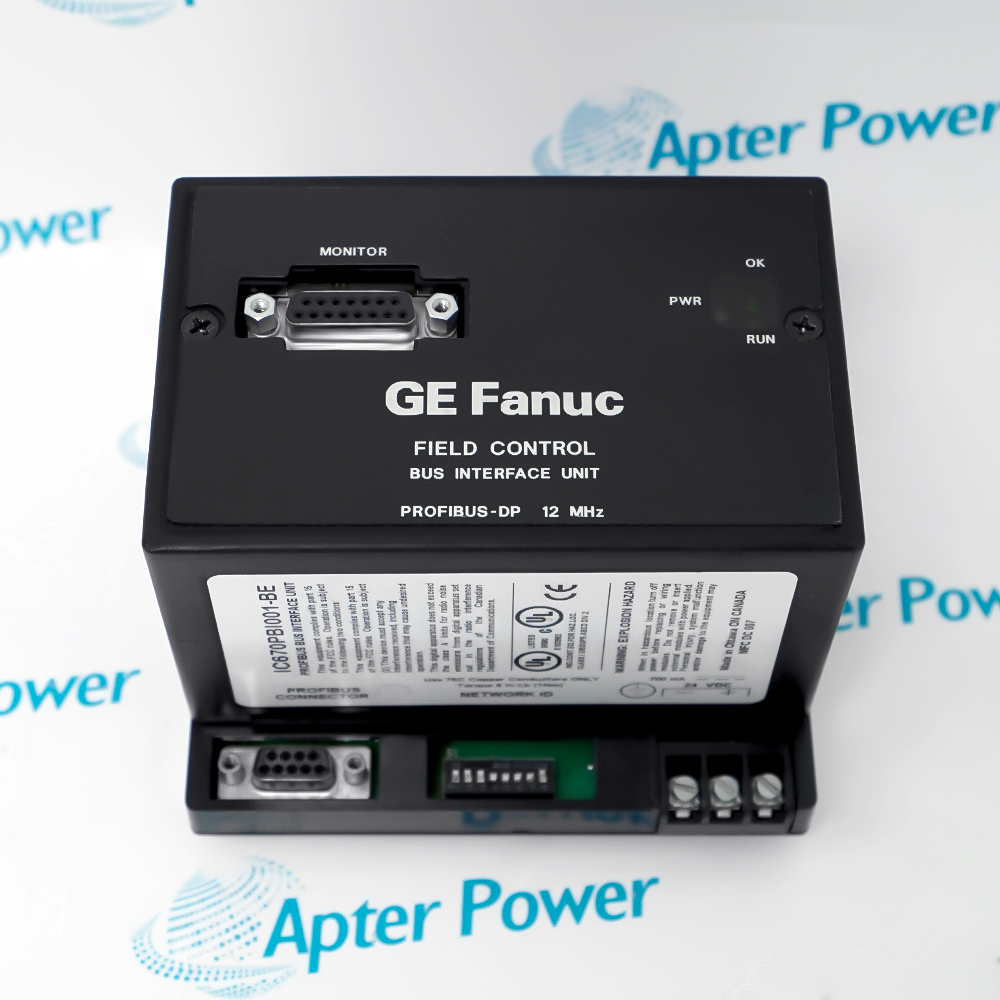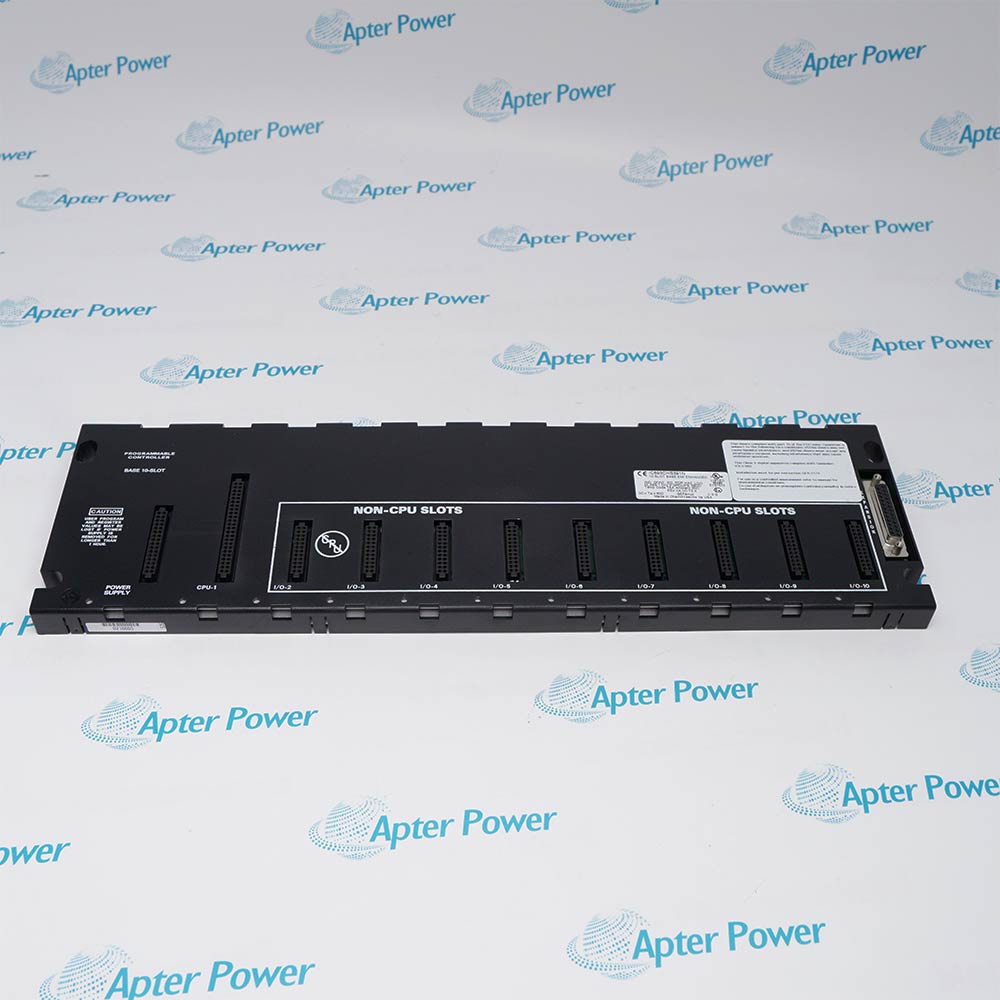
A06B-0104-B111#7000 is installed with matched GE Fanuc servo amplifier, CNC axis-control channel, motor power and feedback cables, machine coupling and holding arrangement.
Engineered applications include Machine-tool feed-axis renewal, Servo motor and feedback-loop verification, CNC axis alignment and direction testing, Installed motion-system restoration.
Important Notice: Match the complete A06B-0104-B111#7000 nameplate, shaft, connector and feedback execution before installation; isolate the servo bus, secure the axis, then prove rotation direction, feedback polarity and travel limits at reduced speed.
The first document consolidates model-specific technical identity and system context. The second provides a separate field workflow for installation, connection checks and commissioning records.
Restores the documented rotary actuator at a configured linear or rotary machine axis.
Confirms power-phase order and feedback direction as one coordinated servo-loop test.
Supports recommissioning after motor, coupling or feedback-cable service.
Provides a controlled path for checking brake, travel limit and axis-reference behavior where fitted.
Verify the complete A06B-0104-B111#7000 marking and the assigned GE Fanuc CNC servo-axis system position before work.
Place the connected machine or process in the approved maintenance state before disturbing A06B-0104-B111#7000.
Isolate the applicable power and field energy, then confirm a safe state before disconnecting A06B-0104-B111#7000.
Record connector, conductor, slot and configuration identities before removal of A06B-0104-B111#7000.
Use ESD controls and protect keyed interfaces, exposed contacts and electronic assemblies during handling.
Confirm that the installed companion hardware and approved project match the A06B-0104-B111#7000 arrangement.
Restore power in a controlled sequence and review device, rack and host diagnostics.
Prove the intended function and retain the final test result before returning A06B-0104-B111#7000 to service.